Clamping · Fixturing · Zero-Point

The fixture is the part of the job nobody quotes

Every dovetail milled, every soft jaw cut, every setup dialled in twice — that is spindle time spent on holding the part instead of making it. We supply the German-engineered clamping that takes that work off the machine, plus the fixturing, clamps and locating hardware that keep a setup repeatable — and on the lathe side, Samchully power chucks that cut jaw changes and jaw boring down to minutes.

Form fitHWR SOLIDStamp stamping station pressing a tooth contour into a blank
SOLIDStamp® stamping
A stamping station presses a defined tooth contour into the blank outside the machine, so the part clamps by form fit on a 3 mm edge instead of by friction — no milled clamping points, and a vise with almost no collision contour.
HWRSOLIDStamp3 mm edgeOff-machine prep
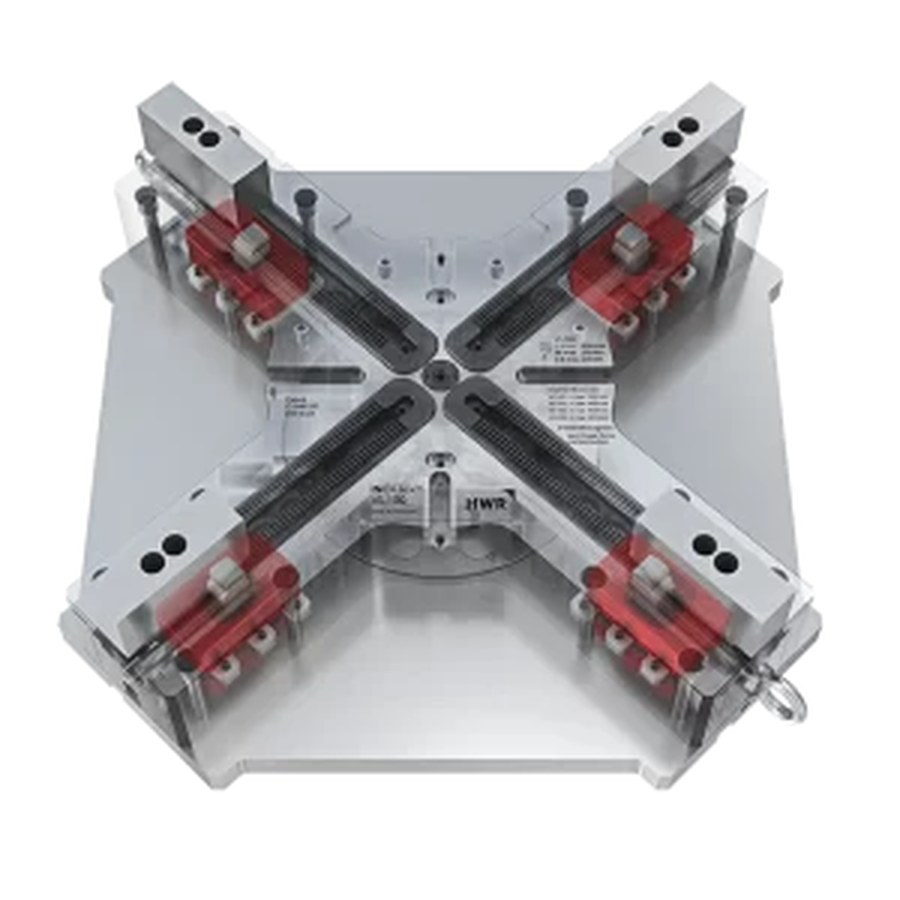
CompensatingHWR INOFlex VL compensating four-jaw chuck with pendulum jaws
INOFlex® VL 4-jaw chuck
All four jaws compensate on two parallel axes, so round, square, rectangular and genuinely irregular parts clamp concentric to the rotary axis. 160–1200 mm, with centrifugal force compensation at speed.
INOFlex VL2 + 2160–1200 mmCFC
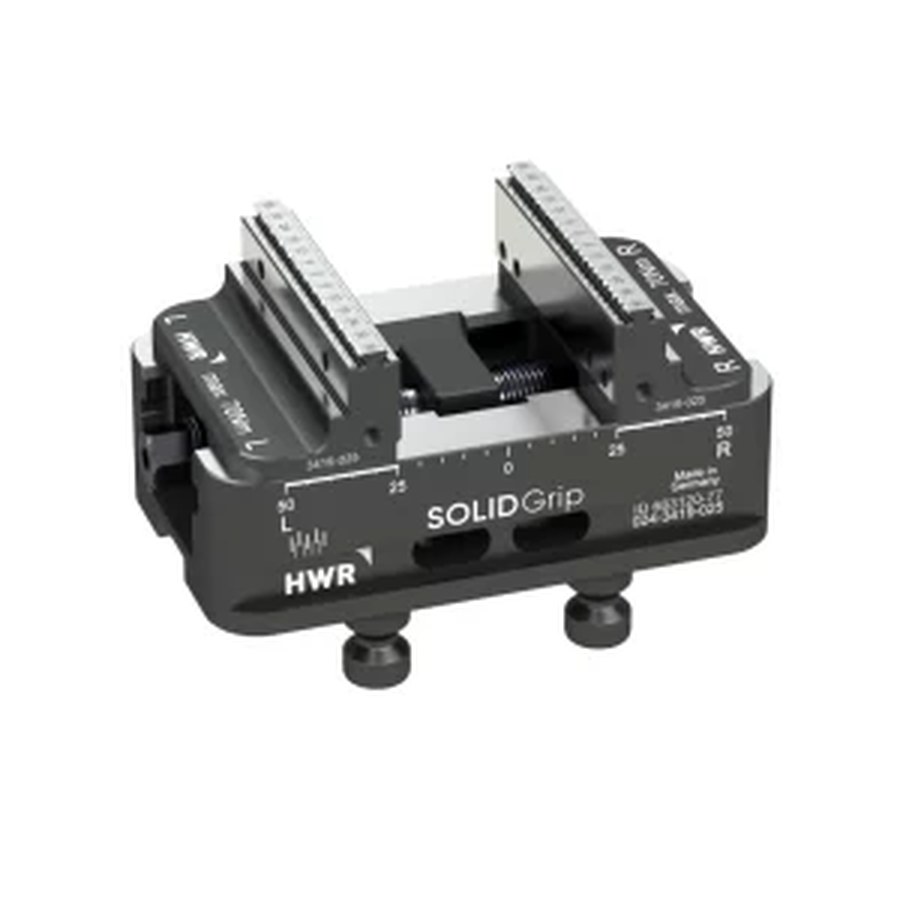
5-axisHWR SOLIDGrip centering vise
SOLIDGrip® centering vise
Self-centering vise with a low, slim body for five-axis work — the part sits high and clear of the jaws so the tool reaches five sides without the fixture getting in the way.
SOLIDGripSelf-centeringLow profile5-axis access
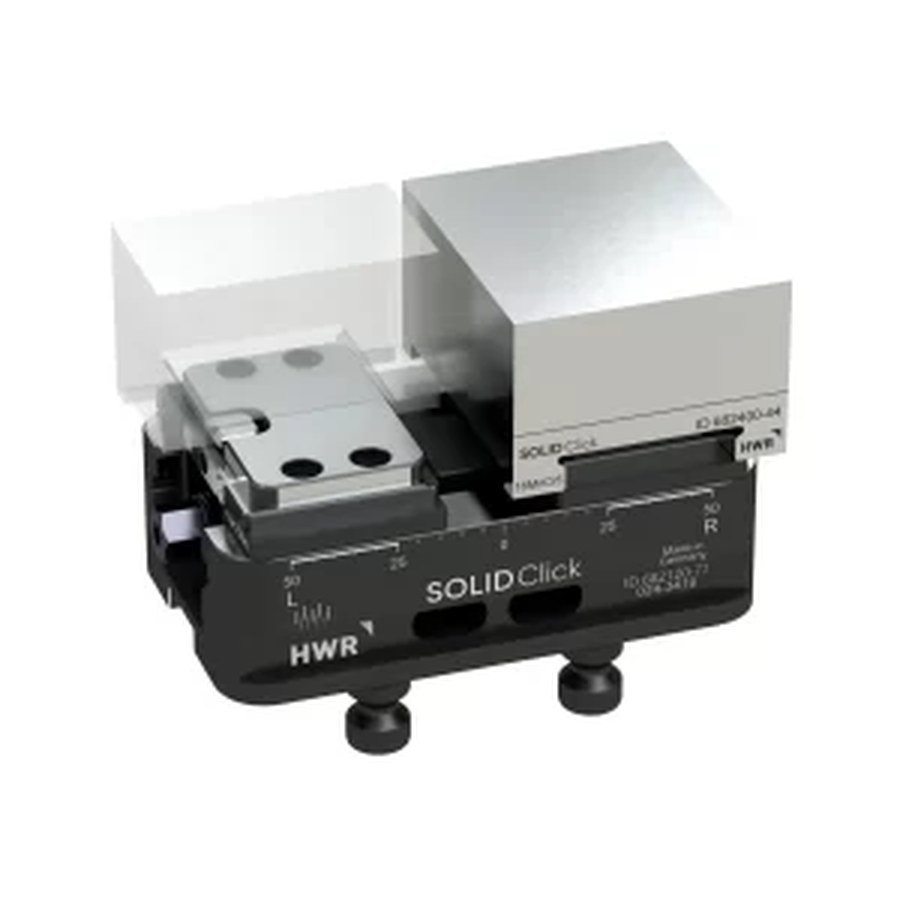
Quick changeHWR SOLIDClick 5-axis vise with quick jaw change
SOLIDClick® 5-axis vise
Jaws that change without tools and without re-dialling — so one vise body covers several jobs and the setup does not have to be proved out again every time the part changes.
SOLIDClickTool-free jawsRepeatable5-axis
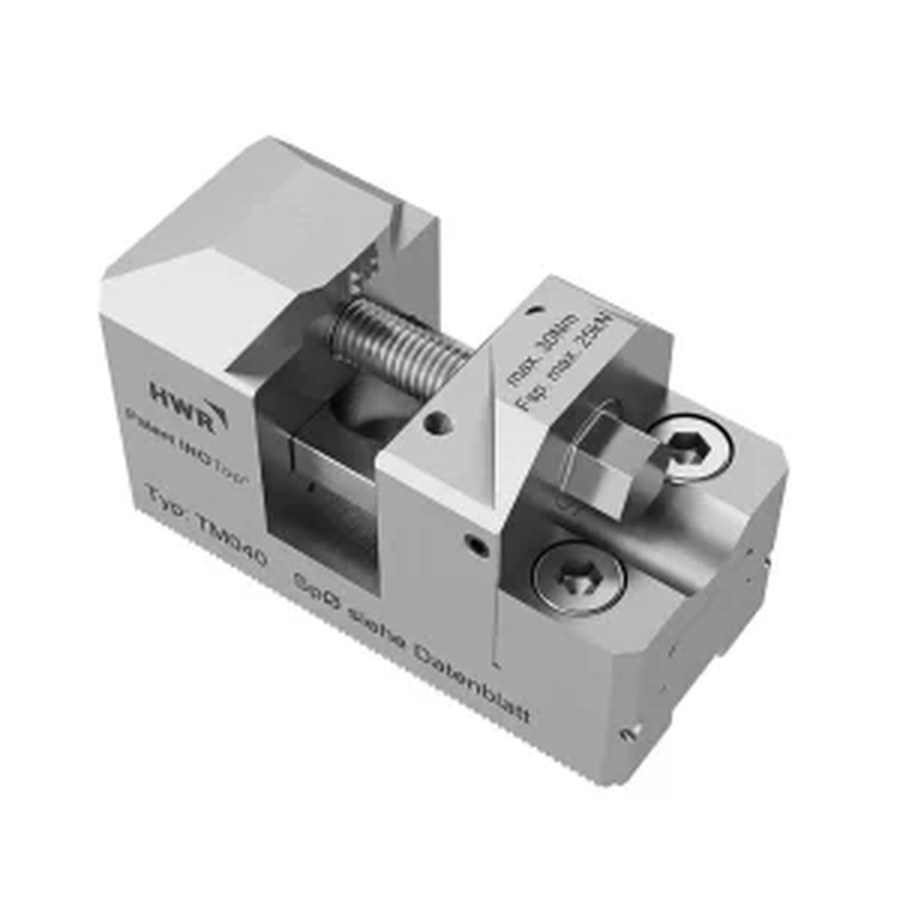
HybridHWR INOTop TM040 hybrid chuck
INOTop® hybrid chuck
A hybrid between a chuck and a vise — the grip and repeatability of a chuck with jaw travel that suits prismatic parts, for shops that would otherwise own both.
INOTopINOLineUNIJawsPrismatic
Zero-point clamping
SOLIDPoint® and SOLIDBolt mechanical zero-point systems — pallets and fixtures that drop in and repeat, with both 96 and 52 mm grids in one plate so adapter plates are not needed.
SOLIDPointSOLIDBolt96 & 52 grid
Fixturing, clamps & locating
Jergens Ball Lock quick-change fixturing and vises; Mitee-Bite low-profile edge and fixture clamps; HALDER ball lock pins, spring plungers and locating elements.
JergensMitee-BiteHALDER
SOLIDLine catalog ↗ All HWR products ↗ Web catalog & downloads ↗ SOLIDStamp datasheet ↗
Workholding · HWR

Hold the part without spending the setup

German-engineered workholding from HWR — two ways to stop losing time and envelope to the fixture. SOLIDStamp moves clamping prep off the machine entirely; INOFlex VL clamps round, cubic and irregular parts concentric in one chuck.

New · HWR SOLIDStamp Stamping Technology

Prep a blank for clamping in seconds

A stamping station presses a defined tooth contour into the blank under high pressure. The part then clamps by form fit rather than friction — so the force-intensive work happens outside the machine, in non-productive time, and the vise can stay slim and accessible.

3 mmMinimum clamping depth · less material bought, less cut away as scrap
Form fitLower clamping pressure with higher holding force · less workpiece deformation, truer parts
SecondsBlanks prepped outside the machine · no milling clamping points before the real work starts
RepeatCenter marking positions parts accurately in series · no stops cluttering the table
Datasheet ↗
HWR · INOFlex VL HWR INOFlex VL compensating four-jaw chuck clamping a part on a 5-axis machining centre
HWR INOFlex® VL · Compensating 4-Jaw Chuck

One chuck for round, cubic and awkward

A conventional chuck drives every jaw around a common centre, so anything that isn’t round is over-determined — it clamps on two points and racks. The INOFlex drive moves on two parallel axes with the opposed slides linked, so all four jaws compensate. Round, square, rectangular and genuinely irregular parts all clamp concentric to the rotary axis, and thin-wall parts clamp without being squeezed out of shape.

2 + 2Compensating centric clamping · or centric on 2 jaws, or against 1 or 2 fixed stops
160–1200mm chuck range · one chuck replaces the 2-jaw, 3-jaw, 4-jaw and vice you were swapping between
Low profileWeight-optimized body and low overall height · more of the trunnion’s rated load left for the part
CFCCentrifugal force compensation · minimal clamping force loss at the top of the speed range
Product page ↗ Datasheet ↗

Video courtesy of HWR Workholding USA · watch on Facebook

Lathe workholding · Samchully

Stop paying the lathe to wait on the chuck

On a turning center, the chuck is where changeover time hides — pulling jaws, boring soft jaws on a ring or slug, dialing back in. Samchully has built power chucks, cylinders and lathe workholding since 1975, and two of their chucks go straight at that lost time. We supply the full Samchully line and help you size the right chuck for the spindle.

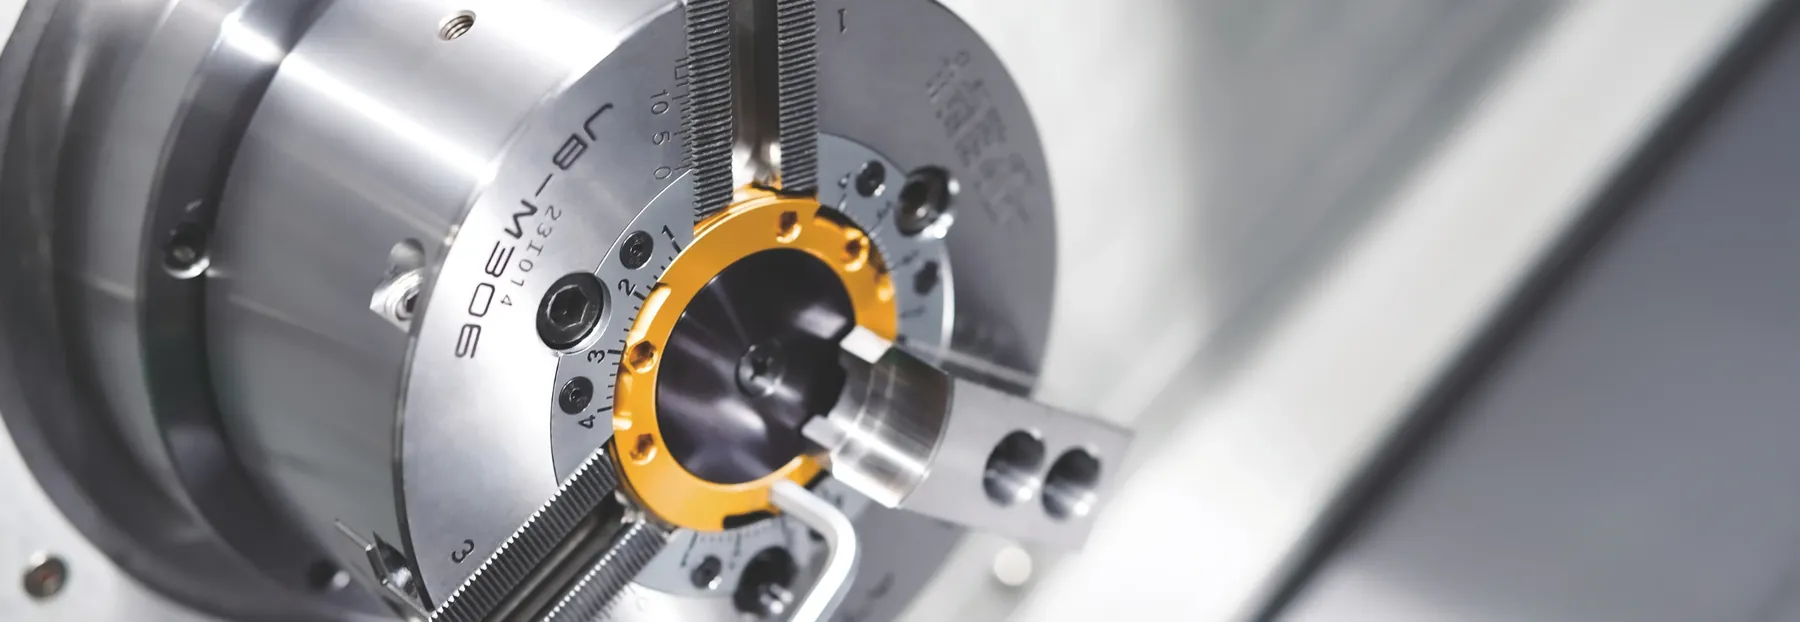
Samchully JB-M306 power chuck with its built-in jaw boring ring set on the spindle, soft jaws gripping a boring plug
Samchully · JB power chuck Samchully JB power chuck with built-in jaw boring ring on a CNC lathe
Samchully JB · Built-in jaw boring

Bore soft jaws without the boring ring

A standard power chuck needs a separate boring ring or slug every time soft jaws are cut — extra parts, extra setup, and a hand in the machine. The JB chuck has the boring ring built in: a rotating sleeve aligned with the master jaws, so jaws are bored right on the spindle. It drops in where a standard HS or MH series chuck mounts today.

0.1 mmBore increments · versus the 1.5 mm serration pitch on a standard chuck, so soft jaws re-bore up to 15× more before replacement
0.0004″Runout with bored jaws · the same accuracy as a standard premium Samchully power chuck
+20%Jaw boring diameter · no ring bolted to the jaw mounting bolts eating capacity
Robot readyJaw boring can be automated · no manual step to stop a lights-out cell
JBM mega-bore ↗ JBH standard ↗

How the built-in ring works

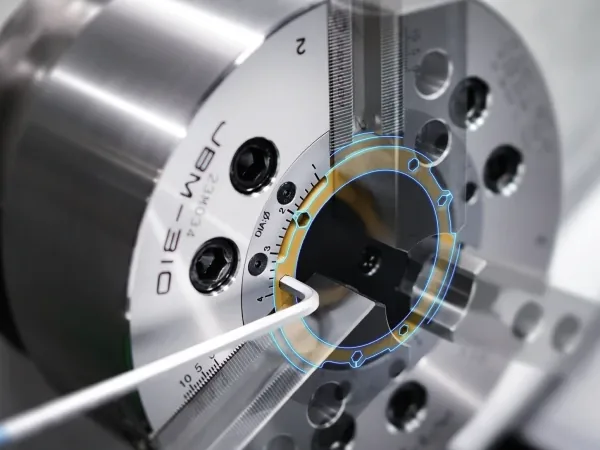
  1. Set the diameter. Turn the gold sleeve with a hex key against the diameter scale on the chuck face — adjustable in 0.1 mm steps.
  2. Close the jaws on the ring. The master jaws grip the built-in ring the same way they would grip a loose boring ring, with no slug to find and no bolts to set.
  3. Bore the soft jaws on the spindle. The ring stays in the chuck, so there is nothing to unbolt, store or lose — and nothing that needs a hand in the machine on an automated cell.

Four details that make the JB faster

Samchully JBM-310 power chuck with its rotating boring sleeve highlighted and a hex key in placeRotating sleeve · JBM-310

A sleeve that sits on the master jaws

Samchully’s proprietary rotating sleeve is aligned with the chuck’s master jaws, so soft jaws are bored on the chuck without a conventional boring ring or slug. Samchully rates it at up to 90% less downtime, by cutting out the calculations and adjustments jaw boring usually takes.
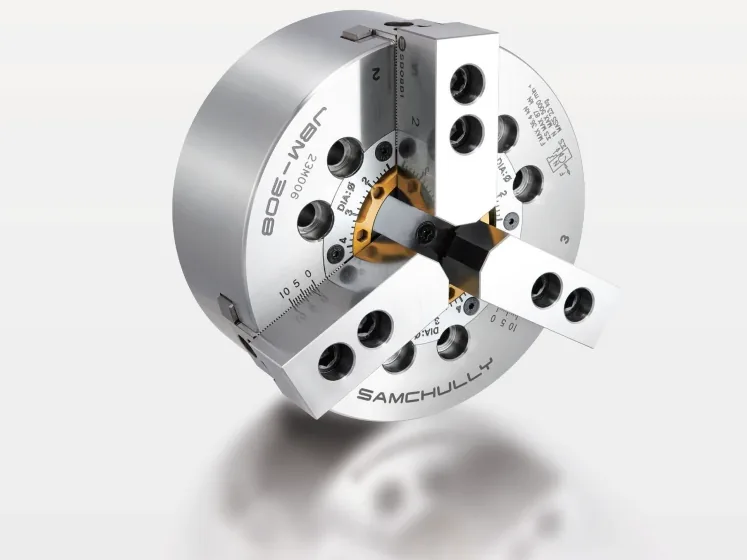
Samchully JBM-308 JB power chuck with three soft jawsJBM-308

One tool: an Allen wrench

No boring rings to buy and no pre-machined slugs to make, store and find. A standard hex-head Allen wrench is the only tool needed to bore the jaws. The design is patented (Samchully patent No. 10-2582103).

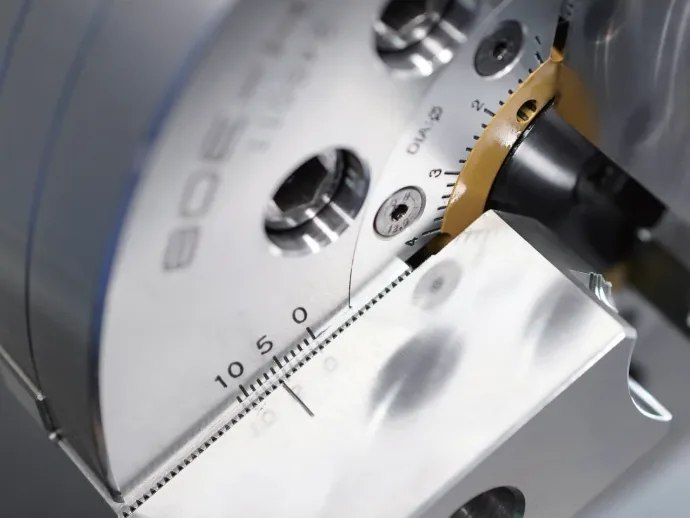
Laser-etched scale on a Samchully JB chuck face lined up with the witness mark on a soft jawScale & witness mark

Every jaw on the same tooth

A laser-etched scale on the chuck face and a witness mark on each soft jaw line all three jaws up on the same serration pitch, so setup is read off the chuck instead of counted by eye.

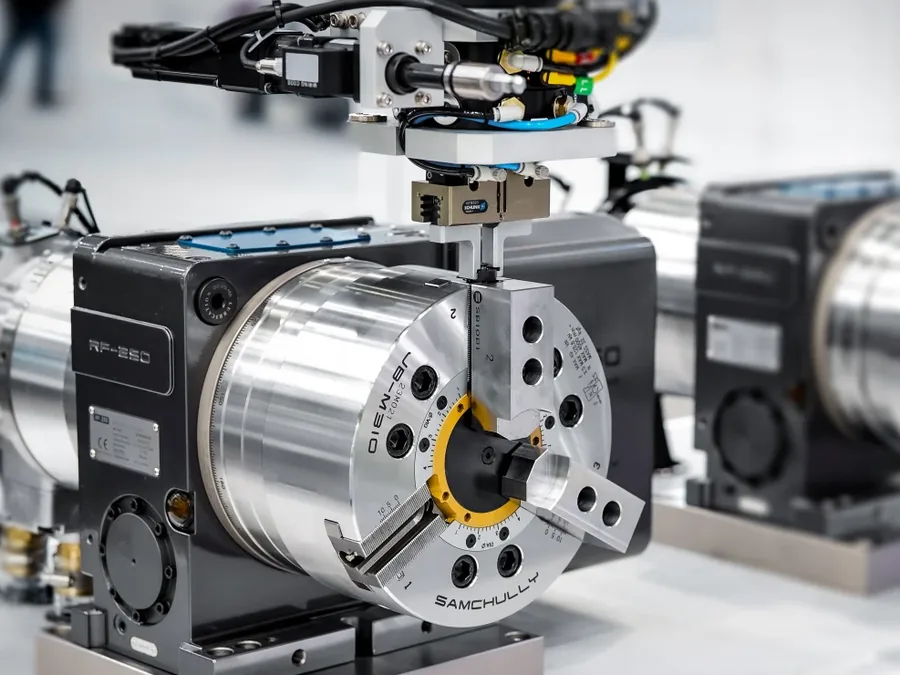
Samchully JB chuck mounted on an RF-250 rotary table under a robot gripper in an automated cellJB chuck · automated cell

Robot ready

Boring jaws on a standard power chuck needs a person at the machine, which is what keeps most chucks out of automated cells. On the JB the boring step can be automated, so it stays inside the automated cycle.

QJC quick jaw change chuck
All three jaws change in under a minute, with no re-boring — repeatability within 0.02 mm. Built for high-mix, low-volume work where part sizes change every shift. 6″ to 24″.
QJC< 1 min0.02 mmReversible jaws
Power chucks & cylinders
Hydraulic power chucks in 2-, 3- and 4-jaw, standard and mega-bore, dimensionally interchangeable with the common 200-series chucks already on your lathes — plus the rotary cylinders that drive them.
HS / MHMega-boreRotary cylinders
Steady rests, jaws & manual chucks
Self-centering steady rests for long or heavy shafts, quick-change and soft top jaws, manual scroll and independent chucks — the rest of the lathe side from one source.
Steady restsTop jawsManual chucks

What is chuck downtime costing you?

Put in your own numbers. Samchully’s published figures are used as the starting point for the new-chuck times — change them if your floor is different.

Estimated savings per year
$0
Spindle hours recovered
0
Downtime value
$0
Payback
Add a chuck price
Run Samchully’s own savings calculator ↗

An estimate for planning, not a quote. New-chuck defaults come from Samchully’s published specs: QJC jaw changes under one minute, and JB bore increments of 0.1 mm versus a 1.5 mm serration pitch.

Samchully catalog ↗ QJC series ↗ Savings calculator ↗

Adding a 4th or 5th axis to a mill? See Samchully rotary tables & trunnions.

Catalog · stamping & zero-point HWR SOLIDLine SOLIDStamp, SOLIDPoint, SOLIDBolt and SOLIDGrip — the full SOLIDLine catalog plus the SOLIDStamp datasheet.
Catalog · chucks & jaws HWR INOLine® INOFlex® compensating 4-jaw chucks, INOZet® pendulum bridge, INOTop® hybrid chuck and UNIJaws® standard clamping jaws.
Catalog · fixturing Jergens Workholding components, Ball Lock quick-change fixturing, vises and clamping — master catalog and brochures.
Catalog · clamps & locating Mitee-Bite & HALDER Low-profile edge and fixture clamps, plus ball lock pins, spring plungers and locating elements.
Machines · Lights Out Machinery
Pulling setups out of the job? The machine matters too.

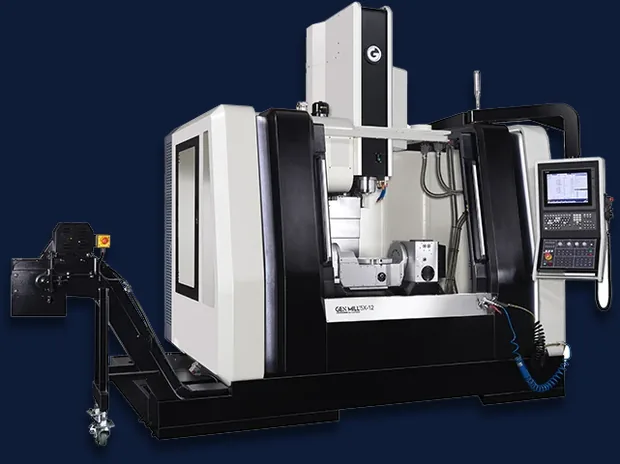
Form-fit workholding pays off hardest on a 5-axis trunnion, where every bit of collision contour costs you reach. Our machinery side runs ten vertical machining centers — GEN MILL 3-axis, 5-axis trunnion and double-column bridge, plus the Hasegawa PM320-5X — from 12.59″ to 63″ of X travel, and quotes the workholding with the machine. Tooling & accessories on LOMA.

See the 5-axis VMCs →
GEN MILL 5X-12 five-axis vertical machining centre with 12 inch trunnion
Get support

Let's take work off your floor

Fighting stockouts, chasing cycle time, tired of a 1-800 catalog, or sizing up new machine capacity? Start a conversation with the independent team that handles all of it.

📞
978-356-2500
Mon–Fri, 7:30am–5pm ET
✉
office@nsitools.com
📍
Ipswich, Massachusetts
Serving New England & the Northeast
🏭
Machines? The machinery side of our team — lightsoutma.com
A real application engineer replies within one business day — or call 978·356·2500 now.